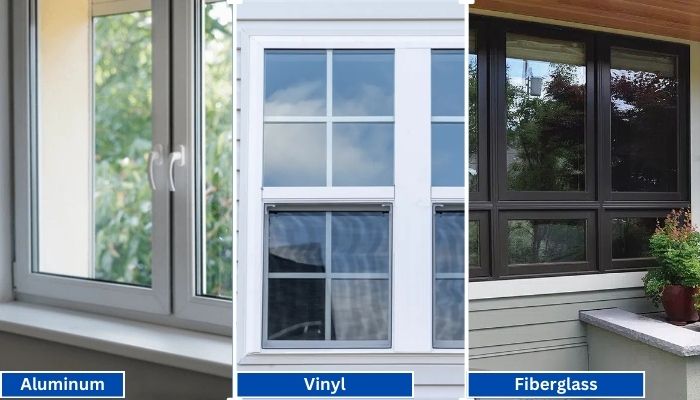
Vinyl generally has the shortest lead times because it is widely produced in standard configurations. Fiberglass is mid-range, especially for factory-painted colors.
Read More
PROUDLY CANADIAN COMPANY OWNED & OPERATED IN TORONTO SINCE 1989!
Vinyl generally has the shortest lead times because it is widely produced in standard configurations. Fiberglass is mid-range, especially for factory-painted colors.
Read More
Vinyl windows have become the go-to choice for homeowners in Toronto, thanks to their durability, energy efficiency, and low maintenance requirements. Whether you're upgrading your home for better insulation or enhancing
Read More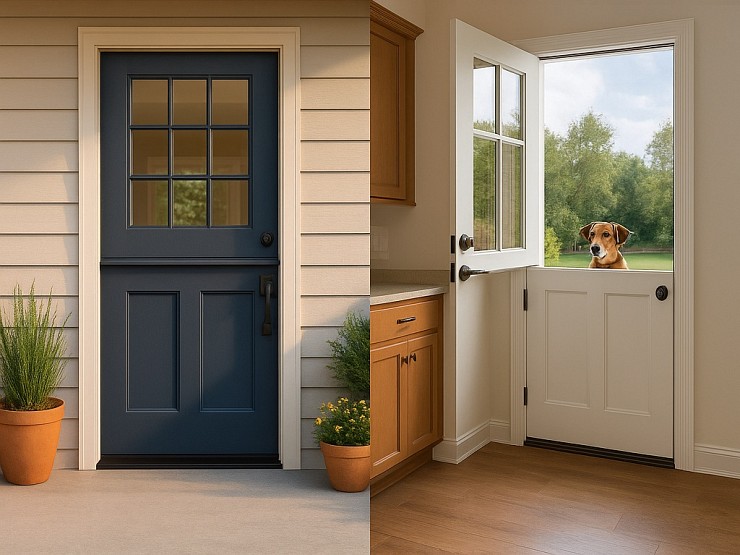
Thinking about changing your front door? A fiberglass Dutch door might have caught your eye. It’s not just a door. It’s part style statement, part smart functionality.
Read More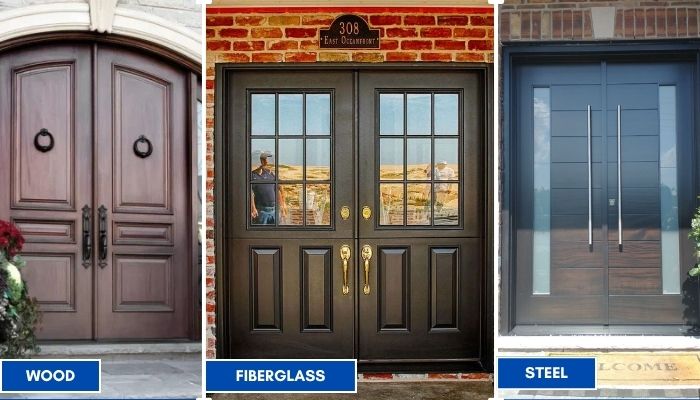
Thinking about replacing your front doors? Double doors are a bold upgrade. They look great, let in more light, and make moving big stuff easier. But the material you choose makes all the difference; especially here in Toronto.
Read More
Thinking of giving your home that cozy, farmhouse charm? Let’s talk doors. Specifically, the fiberglass front doors in farmhouse style. You get the rustic look, without the rot, warping, or constant upkeep that comes with wood.
Read More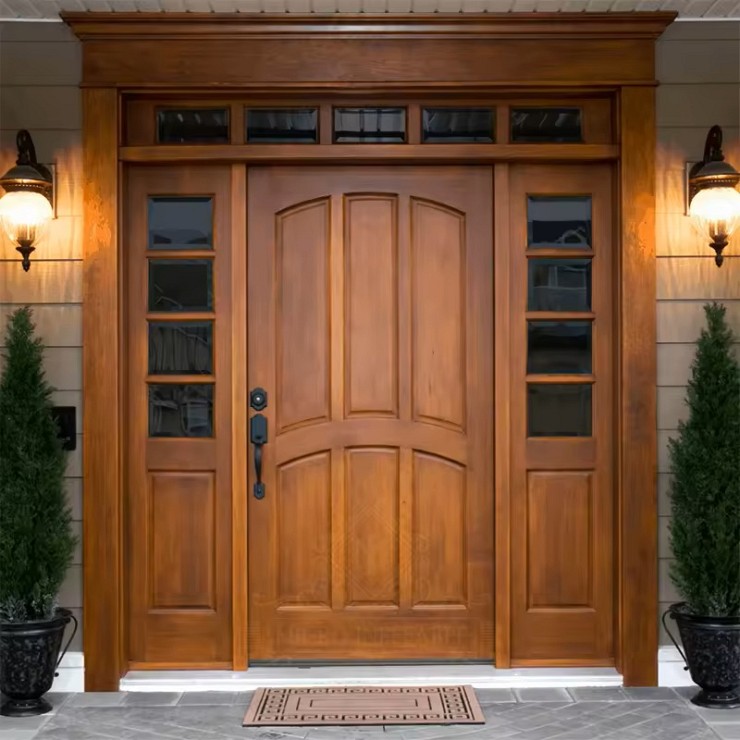
You want something that looks great, lasts long, and doesn’t stress you out with maintenance. You’re not alone. That’s exactly why more and more Toronto homeowners are choosing...
Read More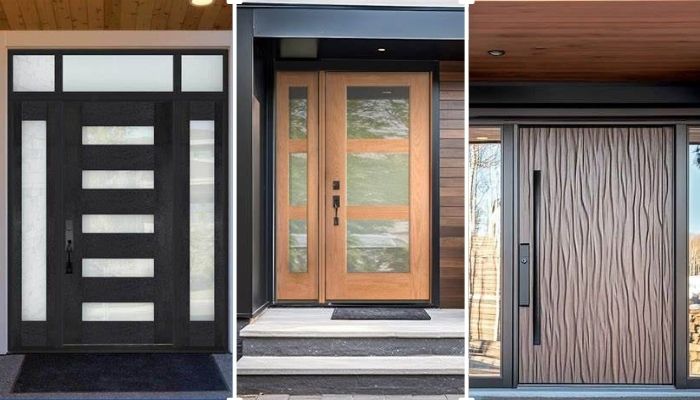
Thinking about replacing your front door? Let’s talk fiberglass. It's one of the smartest upgrades you can make, especially if you're living in Toronto. Whether your current door is drafty, outdated, or just plain boring.
Read More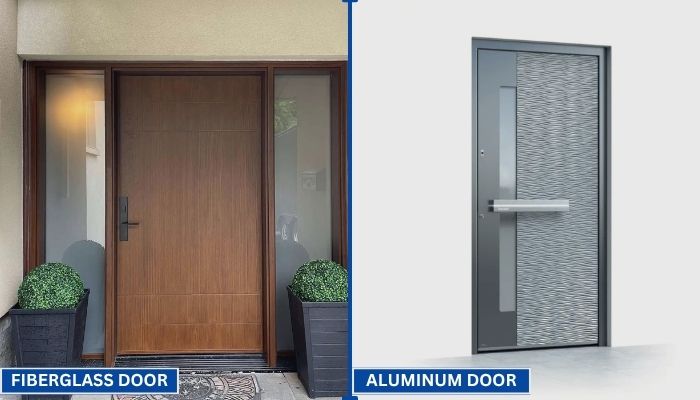
Your front door does more than just open and close. It protects your home, adds curb appeal, and helps control indoor temperature. That’s why picking the right door material matters.
Read More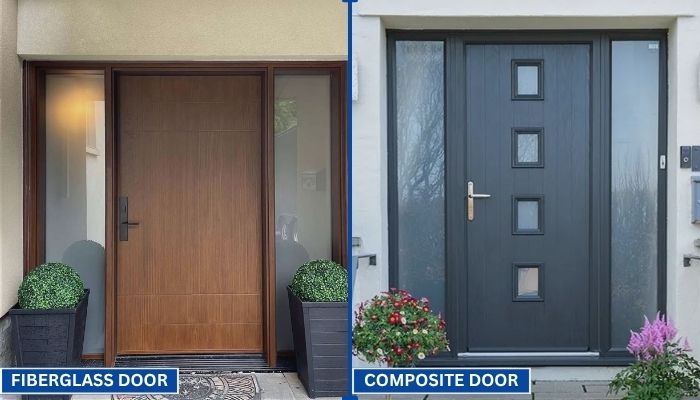
Choosing the right door can be confusing. You want something that looks good, lasts long, and keeps your home secure. Two of the most popular options today are fiberglass and composite doors.
Read More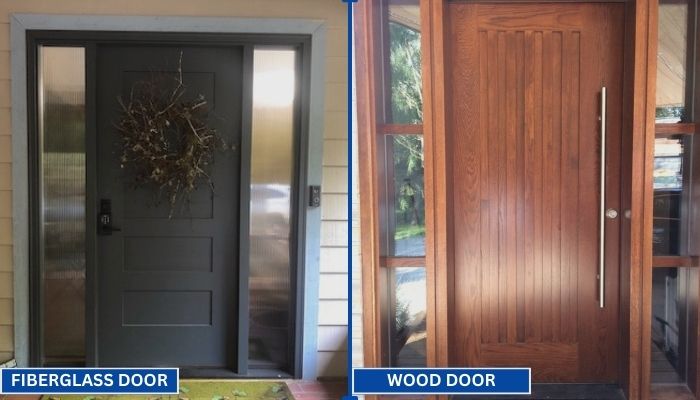
Replacing your front door is a big decision. Wood and fiberglass are two of the most popular materials for entry doors. Each has its own strengths in terms of style, durability, and maintenance. To help you choose the right one for your home, we have to go through a clear comparison.
Read MoreChoosing reliable Grade 304l Stainless Coils suppliers in 2026 requires more than comparing prices. Buyers must examine chemical composition, surface finish, coil tolerances, production records, and delivery consistency. A polished coil may look impressive under warehouse lighting, yet hidden thickness variation can affect forming, welding, and final product quality.
Dr. Harold M. Cobb, a recognized stainless-steel historian and metallurgist, has stated, “Stainless steel is not one material, but a family of materials.” This observation remains practical. Grade 304L is valued for its low carbon content, corrosion resistance, weldability, and broad industrial use. However, suppliers do not offer identical performance. Their melting controls, annealing methods, pickling practices, and inspection systems can differ significantly.
Look closely.
A dependable supplier should provide current mill test certificates, heat numbers, dimensional reports, and clear traceability. Site experience also matters. A supplier serving food-processing equipment may understand hygienic finishes better than a general metal trader. Meanwhile, a construction-focused distributor may offer stronger stock availability and faster regional delivery.
This guide evaluates leading suppliers through technical capability, quality assurance, export experience, customization options, and customer support. It also considers weaknesses. No supplier is perfect, and marketing claims deserve verification. Some companies communicate well but provide limited technical evidence. Others produce excellent coils but respond slowly when specifications change.
The strongest choice depends on your application, not reputation alone. By comparing measurable evidence, buyers can reduce waste, avoid mismatched material, and select Grade 304L Stainless Coils with greater confidence.
304L stainless steel is a low-carbon version of 304 stainless steel. It contains chromium and nickel, which help form a protective oxide layer. This layer supports corrosion resistance in kitchens, chemical equipment, and architectural interiors. That small carbon reduction matters. After welding, 304L is less likely to form chromium carbides along grain boundaries. This helps reduce the risk of weld-related corrosion. Fabrication is more forgiving.
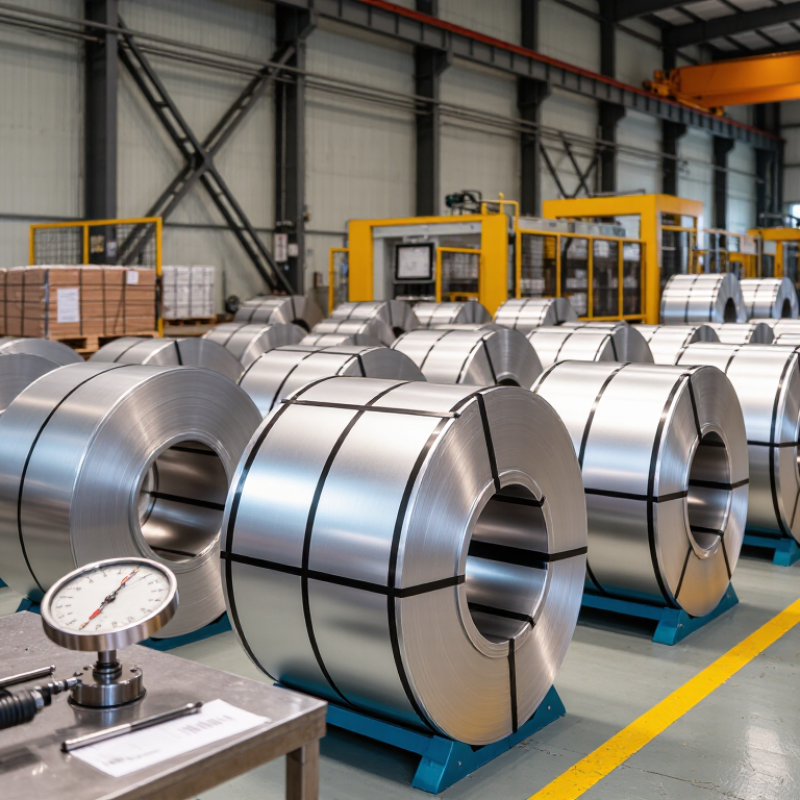
The material is supplied in coils because continuous strip production improves consistency and handling. Coils can be slit into narrow widths or shaped through rollers. They also reduce repeated setup work during manufacturing. A typical coil may show a smooth, reflective surface, controlled thickness, and carefully rounded edges. These details affect stamping, bending, and surface finishing. In practical purchasing, I check the heat number, thickness tolerance, coil weight, and test certificate. A reliable supplier should also explain annealing, pickling, and surface grades clearly.
304L is not perfect for every environment. Strong chlorides can still cause pitting, especially near seawater or stagnant moisture. I have seen material selected by appearance alone, which is a costly mistake. Chemical exposure, forming requirements, and welding methods deserve equal attention. Supplier experience matters here. Clear inspection records and traceable production data often reveal more than a polished sales description. “Top grade” should mean verified performance, not merely a bright surface.
Technical reference and supplier-selection matrix for 304L stainless steel coils
| Evaluation Dimension | 304L Stainless Steel Reference | Why It Matters in Coil Applications | Supplier Documentation or Inspection Point |
|---|---|---|---|
| Material designation | AISI/SAE 304L; UNS S30403; commonly specified under ASTM A240/A240M for plate, sheet, and strip. | Provides a recognized material identity for purchasing, fabrication, and traceability. | Request the material test certificate showing grade, heat number, applicable standard, and product form. |
| Nominal chromium content | Typically 18.0–20.0% by mass under ASTM A240 chemical limits. | Chromium forms a passive oxide film that provides the basic corrosion resistance of the stainless steel. | Verify the heat-analysis result against the agreed standard and purchase specification. |
| Nominal nickel content | Typically 8.0–12.0% by mass under ASTM A240 chemical limits. | Nickel helps stabilize the austenitic structure and supports ductility, formability, and toughness. | Check the certified chemical analysis rather than relying only on the grade label. |
| Maximum carbon content | 0.030% maximum by mass for the “L” low-carbon grade. | The lower carbon level reduces the risk of chromium-carbide precipitation during welding and helps preserve corrosion resistance near welds. | Confirm the carbon result and specify 304L when welding or post-weld corrosion performance is important. |
| Material structure | Austenitic stainless steel; generally non-magnetic in the annealed condition, although cold working can increase magnetic response. | Supports excellent formability and toughness for stamped, rolled, and fabricated coil components. | Request mill documentation for condition and avoid using magnetism alone as a grade-identification test. |
| Density | Approximately 7.9–8.0 g/cm³, depending on reference and composition. | Useful for estimating coil weight, freight requirements, slitting yield, and material consumption. | Compare the calculated mass with the ordered dimensions, theoretical weight, and actual weighbridge record. |
| Typical tensile strength | At least about 515 MPa for annealed sheet and strip under ASTM A240 requirements; actual values vary with product and condition. | Indicates resistance to tensile loading and helps determine forming and processing limits. | Review the certified tensile test results for each heat or lot as required by the purchase order. |
| Typical yield strength | At least about 205 MPa at 0.2% offset for annealed material under ASTM A240 requirements. | Important for calculating forming loads and assessing permanent deformation during service. | Check yield strength, tensile strength, and elongation together; do not evaluate quality from one value alone. |
| Elongation | Commonly specified at approximately 40% minimum in 50 mm for annealed ASTM A240 sheet and strip, subject to the applicable product specification. | High elongation supports deep drawing, bending, spinning, and other cold-forming operations. | Match the test method, gauge length, thickness range, and minimum value to the contract requirements. |
| Surface finish options | Common finishes include 2B, BA, No. 4, and No. 8, depending on the product and processing route. | Surface condition affects appearance, cleanability, friction, reflectivity, and suitability for architectural or food-processing equipment. | Define finish, roughness target where applicable, protective film, inspection lighting, and acceptable surface defects. |
| Common thickness range | Available thickness depends on the mill, standard, rolling route, and order quantity; thin-gauge and heavier coil products are both commercially available. | Thickness tolerance directly affects part dimensions, weight, forming behavior, and downstream slitting performance. | Confirm nominal thickness, permitted tolerance, measurement method, and sampling frequency before order placement. |
| Width and edge condition | Coils may be supplied in mill edge or slit edge configurations, subject to the ordered width and tolerance. | Accurate width and clean edges reduce trimming waste, tooling issues, burrs, and line stoppages. | Specify width tolerance, camber, flatness, edge condition, burr limit, and coil inside/outside diameter. |
| Weldability | Generally suitable for common fusion-welding processes when appropriate procedures and filler metals are used. | Low carbon content helps reduce sensitization risk compared with standard 304 during welding, although heat input and service conditions still matter. | Ask for welding recommendations, heat-treatment condition, and any intergranular-corrosion test requirement relevant to the application. |
| Corrosion-resistance scope | Good general resistance in many atmospheric, food, architectural, and mildly corrosive environments. | Its balance of corrosion resistance, availability, and formability makes it a widely used coil grade. | Require application-specific review for chlorides, seawater, strong acids, high temperatures, or crevice conditions; 304L is not universally suitable. |
| Magnetic behavior after processing | Usually low magnetic permeability when annealed; rolling, bending, and forming can produce some magnetism. | Prevents incorrect rejection of otherwise conforming material when components have undergone significant cold work. | Use chemical analysis and mechanical testing for identification; define magnetic-permeability limits only when functionally necessary. |
| Traceability | Each production heat or lot should be identifiable through records linking the coil to its chemical and mechanical test results. | Supports quality control, recall management, project documentation, and regulatory compliance. | Check heat number marking, coil number, certificate consistency, packing list, and permanent or removable identification. |
| Recommended supplier qualification status | Evidence-based approval | A technically suitable supplier should demonstrate conformity, stable dimensional control, reliable delivery, and responsive corrective action. | Evaluate certificates, sample inspection, surface quality, dimensional capability, packaging, lead time, nonconformance history, and after-sales support. |
We’ll Come To You!
Quality New Windows & Doors. Competitively Priced!
Christine R.
Please, enter a valid value